Capabilities
How a forging plant should describe its process: each step, the equipment class, and the limits buyers need to know.
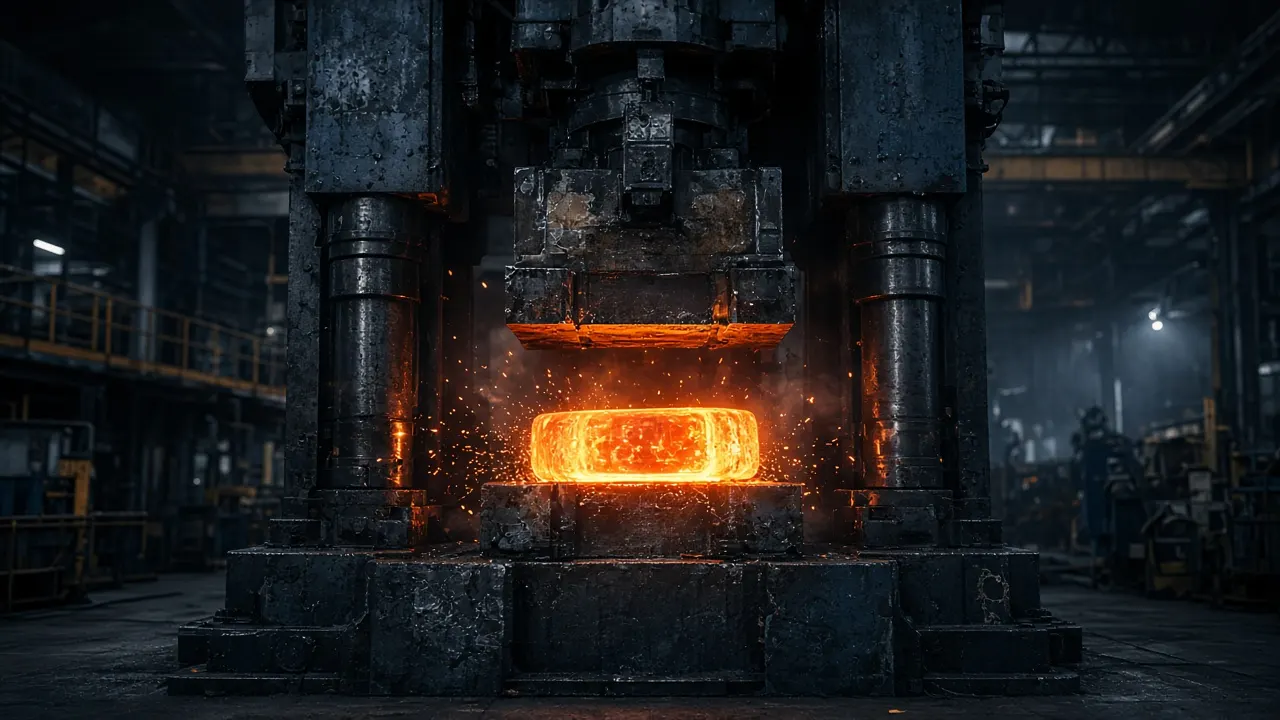
Closed-die and open-die forging
Hot forging on mechanical and hydraulic presses, with in-house die design and die maintenance. Open-die forging for shafts and large blanks; ring rolling for seamless rings.
- Press range 400 – 2,500 t (demo)
- Forging weight 0.2 – 300 kg (demo)
- Induction billet heating with temperature monitoring (demo)
Heat treatment
Normalizing, annealing, quench and temper and solution annealing, with furnace charts kept per batch.
- Batch furnaces and continuous lines (demo)
- Hardness tested on every batch (demo)
- Furnace chart supplied on request (demo)
CNC machining
Rough and finish turning, milling and drilling so forgings arrive ready for assembly or final machining.
- CNC lathes and machining centres (demo)
- Tolerances to IT7–IT9 depending on feature (demo)
- Fixtures designed per part (demo)
Inspection
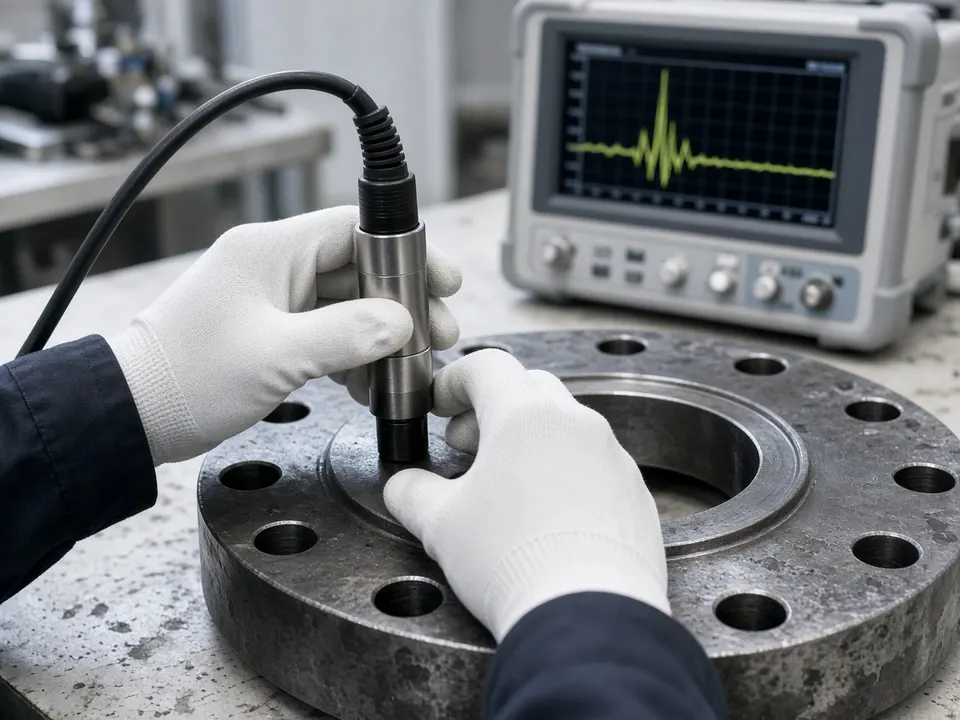
Dimensional inspection, hardness, ultrasonic and magnetic particle testing, and material identification.
- UT, MT and PMI (demo)
- First-article inspection report (demo)
- See the Quality page for documents
Have a drawing? Send it for a demo quotation.
Share your drawing, material, annual quantity and target market. On a real factory site this is where the inquiry goes straight to the sales engineer. On this demo site, nothing is produced or sold.